Recommendations to Select the correct screen printing fabric
5T - 29 T | Overprint varnish, sugar decor on cakes and pastry, sealing pastes, adhesives |
34 T - 49 T | Sports and travelling bags, coarse fabrics, denim, etc. |
49 T - 77 T | Rough, absorbent surfaces, prints on coarse-grained wood, flags and pennants |
68/2 HD | Half-tone printing in large formats, up to approx. 12 lines/cm (30 dots/inch) |
77 T - 100 T | Posters, large lettering, opaque inks, fluorescent inks, coarsely pigmented inks, textured surfaces overprint varnishing |
100 T - 120 T | Half-tone screens up to 20 dots/cm, fine lettering and outlines, solid areas, gauges and dials, sing-printing, self adhesive labels |
over 130 T | Fine line half-tones, step printing, reduced ink deposit |
110 HD and 120 T | Most frequently used in screen printing fabrics for universal applications, electronic printing (ESTAL MONO 'X' ESTAL MONO, ESTAL METAL) |
over 120 T - UV | UV - fabrics with reduced colour volume, especially for printing with UV-inks, also for half-tone printing and very thin deposits with conventional inks, i.e. fine line half-tone screen. |
Object printing (NYTAL)
100 T - 120 T | Printing on plastic bottles and cans, promotional gifts, pens, etc. For coarsely pigmented and opaque inks, i.e. white and yellow |
120 T - 200 S | Fine line half-tone screen, reduced ink deposit for high-speed printing machinery |
120 T-UV-180 S-UV | Especially developed to print with UV-links |
a) Conventional inks
Polyester Mono, Polyester Multi Filament, Polyester Mono Filament
|
Etch resist |
110 HD/120 T |
|
Plating |
90 T/100 T/110 HD |
|
Solder resis 2-comp. |
68 T/77 T 35 pm* 55 T -71 pm* 43 T/49 S +70 pm* |
|
Carbon conductive lacquer |
38 T - 68 T |
|
Marking print |
90 T/100 T/120 T |
|
Removable solder mask |
12 M/12 T/15 T/18 T |
* Build-up of conductor lines (height)
b) UV-inks
Polyester Mono, Polyester Multi Filament, Polyester Mono Filament
|
Etch resist |
140 T |
|
Plating resist |
120 T |
|
Solder resist |
68 T - 120 T |
|
Photo sensitive solder mask |
28 T - 68 T |
Electronic industry (printed circuits)
c) SMD – technique
|
Polyester Mono, Polyester Multi Filament, Polyester Mono Filament |
32 SL/38 SM |
d) Membrane switches
Polyester Mono, Polyester Multi Filament, Polyester Mono Filament
|
Decor foil |
77 T - 120 T |
|
Transparent windows |
100 T - 120 T |
|
UV-structural lacquer |
77 T - 165 M depending on the structure |
|
Adhesive |
36 T - 49 T |
|
Silver conductive paste |
68 T - 100 T |
|
Carbon conductive paste |
49 T - 68 T |
e) Ceramic printings
Theads/cm
|
up to 20 |
Glaze printing, coarse, embossed effect |
|
20 - 62 |
Glaze printing, medium fine |
|
62 - 100 |
In-and under-glaze colours in direct printing |
|
68 - 77 |
Metallic inks |
|
77 - 165 |
In-and under-glaze colours in decalcomania |
|
90 - 100 |
Burnished gold |
|
100 - 165 |
Superimposed and in-glaze colours in half-tone print/especially low-colour deposit |
|
120 - 168 |
Bright gold and lustre preparations |
|
12 - 24 |
Cover coat (film solution) |
|
24 - 34 |
Cover coat in general |
|
Nylon Mono Polyester Mono Filament |
For direct printing with flat screens |
|
Polyester Mono Filament Polyester Multi Filament |
Flat screens |
|
Polyester Mono Filament Polyester Multi Filament |
Decalcomania |
f) Glass printing
Theads/cm
|
40-100 |
Glass printing in general |
|
100-120 |
Ampoule, cosmetic bottles, etc. |
|
43-68 |
Concealing borders on automobile windows (solvent based inks) |
|
90-100 |
Concealing borders on automobile windows (UV-inks) |
|
77-165 |
Rear window heating (silver paste)* |
|
100-120 |
Antennas |
|
40-62 |
Front panels for household equipment (masks) |
|
77-100 |
Front panels for household equipment (contour/half-tone) |
Textile Printing
Polyester Mono Filament
|
19 T - 34 T |
Terry cloth, fur imitations, heavy decor fabrics, denim, printing of flock adhesive |
|
34 T - 49 T |
Decor fabrics, large areas, over-prints, table cloths |
|
43 T - 55 T 34 T - KS 40/2 HD 43 T - KS |
Smooth fabrics, large areas, over-prints |
|
49 T - 62 T 34 T - KS KS 45 T - KS |
Small areas, motives without fine details, also on thick synthetic materials |
|
55 T - 77 T 43 T - KS 55 T - KS |
Coarse half - tones and contours on coarse materials |
|
55 T - 77 T 43 T - KS 55 T - KS |
Fine half tones and contours on smooth and light materials, especially synthetics |
|
68/2 HD |
Recommended for the printing of very light and porous materials which absorb little colour |
|
77 T - 120 T 55 T - KS |
For fine details, half-tones and contours on light fabrics, especially synthetics |
Special applications
T-Shirt printing – direct
Polyester Mono Filament
| Polyester Mono Filament 40 T – 55 T | Main number for lettering and surfaces |
| Polyester Mono Filament 55 T – 62 T | Fine contours |
| Polyester Mono Filament 55 T – 77 T | Single and multi – colour half – tone jobs We recommend Polyester Mono Filament GOLDORANGE |
| Polyester Mono Filament 49 S | A universal fabric |
Flock printing direct
| Polyester Mono Filament 18 T – 32 T | Flock adhesive |
| Polyester Multi Filament 32 SL or | Multi – colour process |
| Polyester Mono Filament 26 S | (flocking through the screen) |
Puff-up colours
| Polyester Mono Filament 21 T – 49 S | according to the desired puff effect |
Flock printing – Transfer
Flock printing – Transfer
| Polyester Mono Filament 40 T – 49 S | For colour printing |
| Polyester Mono Filament 20 S – 29 T | for adhesive printing |
Plastisol printing – Direct
| Polyester Mono Filament 55 T – 77 T | for areas and lettering |
| Polyester Mono Filament 77 T – 100 T | for contours and half-tones |
Plastisol printing – Transfer
| Polyester Mono Filament 34 T – 43 T | for areas and lettering |
| Polyester Mono Filament 55 T – 77 T | for contours and half – tones |
| Polyester Mono Filament 32 T – 40 T | for over print |
Transfer printing – Sublimation inks
| Polyester Mono Filament 77 T – 100 T | area printing on transfer release paper with special inks |
| Polyester Mono Filament 100 T | fine lines, half – tones on transfer relesase paper |
Glitter printing
| Polyester Mono Filament 7 S – 26 S | Printng of glitter paste (mesh number according to size of glitter particles) |
- The synthetic yarns offered for the garment and upholstery trades (curtains, furnishing fabrics, carpets), as well as the cheaper stencil fabrics, used to some extent for screen printing textiles, are all of multifilament (multiple – stand) yarn. Similarly, the natural silk screen fabrics formerly used almost exclusively in screen printing are also multifilament. The best screen printing fabrics, whether of polyamide (nylon) or polyester (Terylene, Dacron, Tergal, Terital) are all woven from monofilament (single – strand) yarns.
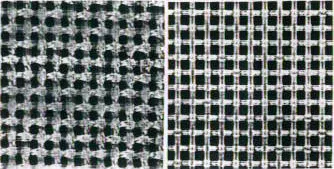
- Owing to the lower abrasion resistance and the multifilament composition, multifilament yarns in stencil gauzes are usually thicker than the corresponding monofilament yarns. Multifilament fabrics for stencil printing are consequently woven only to 77 or 90 threads/cm linear for higher counts that free printing area would be too small and ink penetration inadequate.
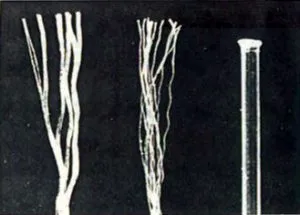
- Screen printing fabrics of monofilament yarns, on the other hand, can be woven up to 200 threads/cm linear even at these fine counts, the free printing area is still satisfactory.
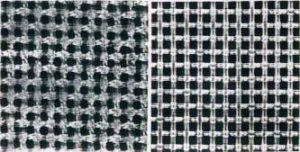
In monofilament stencil fabrics ink penetration is better owing to the compact surface, than in multifilament fabrics on which ink residues remain between the individual filaments and are difficult to remove. Cleaning and re-use far easier with monofilament fabrics than with multifilament weaves. Multifilament gauzes are onluy re-useable with restriction weaves. Multifilament gauzes are only re-useable with restriction. For these reasons it is not surprising that stencil fabrics of multistrand, manmade yarns have hitherto failed to make any headway against monofilament fabrics. Screen printer clearly prefer monofilament fabrics. Screen printers clearly prefer monofilament gauzes. Our monofilament screen printing fabrics are obtainable in a wide range of numbers, between 2 and 200 threads per cm.
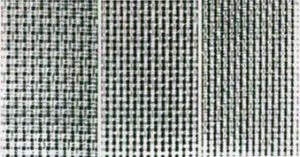
- The fabric number corresponds to the amount of threads per centimeter. The numbres 77 to 180 are very widely used in screen printing. The most popular number are 110 and 12.
- Most of our monofilament fabrics are made in a lighter and in a heavier grade ; in fact many fabric number are produced in various graduations.
- Consequently, a thinner or thicker ink deposit can be obtained by selecting a fabrics of thinner or thicker yarn. Note the technical data in our technical data sheets and price lists.
- n other words, the same fabric number, containing the same amount of threads per centimeter, is woven with thinner or thicker threads.
- The screen printing fabrics, therefore, are produced in the same number in 3-4 grades or qualities.
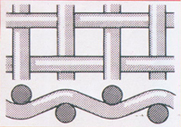
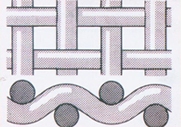
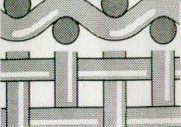
- Polyester Mono Filament, the classical screen printing fabric is made of monofilament (single strand) polyester yarn. Polyester Mono Filament has a higher abrasion resistance than the multifilament polyester fabrics hitherto used in textile screen printing (e.g. Terylene, Dacron, Terital, Trevira, Diolen, etc)
- Polyester Mono Filament has a very high resistance to stretching adn thus ensures and exact register.
- Polyester Mono Filament remains uninfluenced either by usual temperature fluctuations or by humidity, So that the same exact register is maintained from beginning to end of the printing process.
- Polyester Mono Filament is indispensable for large-size printing, in particular for half-tone printing. In very many cases, Polyester Mono Filament can replace the usual stainless steel fabrics, especially in the production of printed circuits, as well as being suitable for the printing of qualioty lablel work.
- Polyester Mono Filament fabrics are made of first grade, electronically controlled polyester monofilament yarn and have the following advantages over metalwire fabrics: A good abrasion resistance and appropriate elasticity despite high stretch-resistance. Metal suffers from Polyester Mono Filament allows long printing runs and permits sharp outlines down to the very last prints. Unlike bronze and steel wire cloths Polyester Mono Filament is rust- and corrosion-proof and much cheaper than stainless steel wire cloth. Polyester Mono Filament is highly wear-resistant and thus more economical than wire cloth. Whereas wire cloths esaily crinkle, develop bagging and other defects, Polyester Mono Filament fabrics are insensitive to impact and pressure.
- Polyester Mono Filament fabrics can be repeatedly stripped and re-used in screen printing.
- Due to its smooth surface Polyester Mono Filament guarantees best in penetration.
- In Screen printing, ink consumption depends principally on fabric thickness and is much reduced by using Polyester Mono Filament fabrics with their finer threads. This considerably shortens the drying time. Efficient work, especially on high-speed automatic machines, urgently requires shorter drying times.
- Polyester Mono Filament lifts off readily from the printing base, avoiding ink smear, and allows the press to be run at higher speeds.
- Polyester Mono Filament is stretched, cleaned and further processed in the same manner as the Nylon Mono Fabrics, but allows an elongation of approx. 3% only (as against 3% to 6% for Nylon Mono), depending on the fabric numbers.
- Polyester Mono Filament is available in various widths: 105 cm, 122 cm, 132 cm, 145 cm, 155 cm, 165 cm, 178 cm, 205 cm, 220 cm, 250 cm, 270 cm, 315 cm, some numbers up to 370 cm.
- Polyester Mono Filament is highly acid-proof and not light sensitive.
After stretching, the screen printing fabric is mounted on a stencil frame. The permissihble tension depends on the tearing strength of the particular fabric.
The resistance to stretching of a particular fabric is a second important factor in ensuring correct register and in determining the proper distance between screen and printing stock. The tension is measured in Newton per cm (1 N = 0,102kp) with mechanical or electronic equipment which one places on the fabric. Optimum tenisoning force for different fabrics The optimum stretching force to be applied in kg/per cm of selvedge depends, as said before on the tearing strength and stretching resistance of the particular fabric.
Modern, monofilament (single-strand) and multifilament (multiple-strand) synthetic weaving yarns have a higher tensile strength than for instance natural silk. Nylon and polyester are nearly alike ; in the thicker yarns polyester is slightly stronger than nylon, while in the finer counts nylon is slightly stronger.
On the other hand, polyester yarn, and to some extent also natural silk, is more stretch-resistant than nylon, however much the nylon is per-stretched and stabilized. Apart from this difference between the tearing strength and the stretching resistance of different yarn materials, for one and the same material it may be stated in principle that bothe these values will be roughly proportional to the cross-sectonal area of the yarn.
The cross-sectional area of a round yarn thread is obtained by the radius or .785 X diameter squared. This means that a round thread A of double the diameter of another thread B of the same yarn material will be about four times as strong in tearing and stretching. With increasing thread diameter, therefore, the strength values increase according to their squares. As we know, stencil fabrics are made in different degrees of fineness (counts).
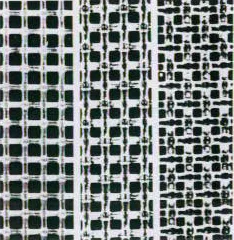
- The count represents the number of threads per cm linear. The counts most used for graphic screen printing are from No 77 to No 165; for special uses, e.g. very fine half-tone printing, up to NO 180. The standard count is No 120. Consequently, the higher the fabric number, the finer the yarn to be used. Moreover, in the same weave counts (same number of threads per cm linear count), fabrics can be woven of thinner or thicker yarns.
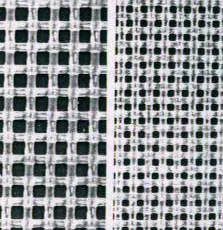
- Considering any of the three fabric grades of the same count illustrated above, i.e. fabrics with the same number of threads, it is obvious that the grade HD with the thicker yarn is stronger than grades T and S with the thinner yarns. This should be taken into account when stretching on printing frames. Thicker, and consequently stronger fabrics can and should be more highly stretched than thinner and lighter fabrics. In pneumatically operated stretching appliances, the air pressure should be increased for stronger fabrics while more care is needed for the lighter fabrics.
Loss of tenison
As mentioned before, it is a well-know fact that loss of tension of a newly stretched screen amounts to approx. 10-20% within the first few hours, depending on the type of tensioning device used, the original mesh tension, the frame stability and waiting time before gluing.
For printing jobs with accurate register, therefor, it is recommended to let the screens rest for a few hours before stenciling. When stretching frames, please take into account this loss of tension. We recommend to use the SST-Newtontester whenever high accuracy of registration is required. For multi-colour work all screens should show the same tension.
A check with the SST-Newtontester, therefore, is especially important. Practical experience has shown that variations in screen tension of 1 to 2 N on the same or different screens are without noticeable influence upon precision in screen printing.
During long print runs of after several screen reclaimings the loss of tension can amount to several Newtons. Please take care that accurate measurements can only be attained if the SST-Newtontester is placed away from the screen frame and the tensioned screen lies on a horizontal plane.
Adhering screen printing fabrics onto the frame
1 Frames
Note: should be taken of the preceding section on printing frames. We can summarize this as follows:
The side of the frame to be gued must first be cleaned. Ink and adhesive residues must be removed and sharp edges and corners of the frame rounded offf. Certain adhesives can be left on the frame if the same adhesive is to be used again and if the coating already applied is sound and flat.
It is always advisable to roughen the adhesive surface of metal, in particular aluminium, using an emery wheel or emery disc of rough grain. Sand-blasting of the surface to be glued is also a good method.
Metal frames should be thoroughly degreased, shortly before gluing, with a suitable solvent (cellulose-thinner, acetone, refined petrol or alcohol).
On aluminium frames the oxygen contained in the air causes an oxide skin to be formed after a short time. Oxidation will even be increased by the use of alcali or by an anodizing process. The surface of the aluminimu is made porous which improves adhesion. In the case, however, where the surface was mechanically roughened, the indentations are etched away to a certain extent by the oxidation, and adhesion is not improved.
In order to stop oxidation it is advisable to cover the roughened surface by means of a two-component adhesive, such as COLESTAL. A frame protected in such a way can be left for a long period. The subsequent coat of adhesive applied during the actual stretching operation bonds perfectly with the precoated frame.
A stencil brush with medium hard bristles should be used. It should be half as wide in diameter as the width of the frame.
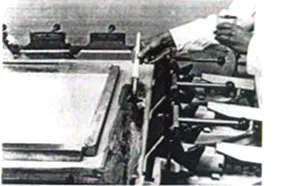
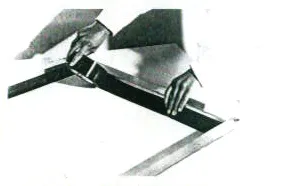
In case of poor contact between mesh and gluing surface of the frame, we recommend placing weights made of 30 X 30 mm iron bars (see picture).
Roughening new fabrics:
For indirect stencils (photo film and carbon tissues), we recommend roughening the surface of new fabrics, nylon or polyester monofilament, once only with Silicon Carbide No. 500 or finer. Rinse the fabrics and mark those frames. The silicon carbide is supplied by the screen printing dealer in 1-kilogramme packs and is applied to the printing face of the gauze with a wet sponge, rubbing for 1-2 minutes. Wash off with high-pressure water-jet
Do not use domestic scouring powders! Such scouring powders are usually not of any standard grain size, so that scouring particles of larger size may clog the fine -mesh fabrics, particles of larger openings and later cause pinholes or cut the threads of the mesh.
Moreover, the chemical additives in house hold scouring powders prevent the adhesion of carbon tissues and films; whereas the silicon carbide powders are thoroughly degreased and chemically cleaned.
Metacresol 1:10 solution in ketone), on the one hand, weakens the nylon filament to an uncontrollable extent, and, on the other hand, does not roughen polyester fiber. We advise against the use of metacresol.
Printing requirements:
Lines
Sharply defined are attained with a coating build-up of 10-18 pm on fabrics with 90 threads/cm and finer.
Rule-of-thumb for coating build-up: approx. 15-25% of the fabric thickness.
Half-tones
The thineest possible coating build-up of 4-8 pm results in thin ink deposit required for half-tone prints.
Rule-of-thumb : approx. 10% of the fabric thickness.
UV-inks
When printing with UV-inks, the ink deposit should generally be as low as possible. As a rule, the coating build-up on the print side of the screen should not exceed 5 pm.
In most cases the basic coating is done wet-on-wet. After intermediate drying, additional coatings are applied in order to eliminate the unevenness of the fabric structure.
The fineness and the quality of the fabric are the determining factors for the number of based coatings of the stencil.
Finess of fabrics
|
Threads/cm
|
Mesh Opening
|
Open area
|
Fabric thickness
|
|
Polyester Mono Filament 120 T
|
45 PM
|
30%
|
61 PM
|
|
Polyester Mono Filament 150 T
|
30 PM
|
20%
|
64 PM
|
|
Polyester Mono Filament 180 T
|
23 PM
|
17%
|
62 PM
|
These examples clearly depict the different percentages of open area in fabrics of similar thickness. The larger mesh opening causes more emulsion to be pressed through the fabric per coathing. In order to attain the same coating thickness on all three fabrics the number of coatings will vary.
The various fabric qualities in the same number also influence the coating thickness, because not only the mesh opening but also the fabric thickness differ.
|
Quality of fabric
|
Mesh Opening
|
Open area
|
Fabric thickness
|
|
Polyester Mono Filament 120 S
|
49 PM
|
37%
|
53 PM
|
|
Polyester Mono Filament 120 T
|
45 PM
|
30%
|
61 PM
|
|
Polyester Mono Filament 120 HD
|
|
Quality of fabric
|
Mesh Opening
|
Open area
|
Fabric thickness
|
|
Polyester Mono Filament 120 S
|
37 PM
|
53 pm
|
2 + 2
|
|
Polyester Mono Filament 120 T
|
30 PM
|
61 pm
|
2 + 3
|
|
Polyester Mono Filament 120 HD
|
22 PM
|
66 pm
|
2 + 4
|
The coating of the screen should be done immediately after degreasing, in order to avoid the fabric from getting soild (dust, etc.); exception : storage in dustfree surroundings.
Stencils for half-tone printing
Avoidance of moire effect
The correct half-tone screen rulings and fineness must be slected according to the size of the print and the distance at which it will be viewed.
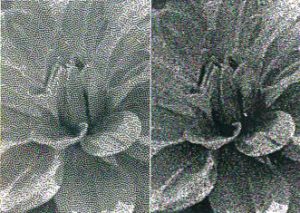
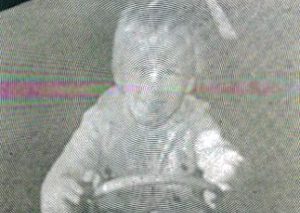
Due to the uneven structure of the screen element, there is no moire effect as with line, dot or bead-string ruling.
Since many years there is in textile printing a kind of graining known as the “DIRACOP method”. For this method the diapositives are prepared, even today, manually, through the use of transparent foils with a grained surface in order to attain the half-tone structure.
In photography the graining effect is attained through the use of a magenta contact screen.
Line ruling is often particularly suitable for the representation of engineering objects in monochrome.
Circular rulings are suitable for monochrome printing: they subconsiously lead me eye of the beholder to a particular image point ; the centre of the circle.
The ordinary dot ruling 4-figure symmetry has nearly 50% coverage with nearyl square dots; in the lower and higher percentage values, dots tend to be circular shaped.
This form of ruling has nearly 50% coverage value, tend to combine in beadlike strings. This results in softer transitions than with square dots. which at more than 50% coverage, combine in both directions. Bead rulings, for instance, are suitable for portraits or for the reproduction of a porcelain effect.
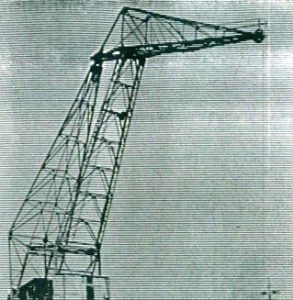
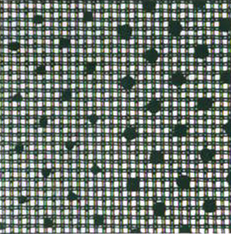
1.The fineness of the half-tone ruling is always linked with the fineness printing gauze and the type of stencil.
The finest details should properly adhere to the gauze. The areas with the highest coverage of ink, especially where the samllest dots of the emulsion must cling to the fabric, are particularly critical. The smallest dots should not rest on one thread or even fall through the mesh opening.
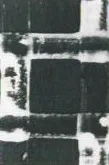
25-line per cm half-tone stencil on Polyester Mono Filament No. 100 HD (magnified 23 X)
Strictly speaking, the diameter of the smallest half-tone screen opening on the diapositive should be microscopically measured in order to slect the gauze of the correct fineness.
In the above example, the fabric is four times finer than the half-tone ruling. It is logical that this fineness is not sufficient for a 94% coverage (which, one must admit, is hardly ever necessary in screen printing). For an 87% coverage it is barely sufficient.
(The relation of the printed half-tone coverage to the 100% coverage is know as tone value.
2. Screen printing is a print-through process and not-as offeset – a transfer process. The screen fabric of the stencil causes a thicker ink deposit than a lithoplate. This is the characteristic and advantage of screen printing, namely, the intense and effective depth of colour.
In hlaf-tone printing, however, the ink deposit should be relatively thin, because, the finer the half-tone ruling and the higher the degree of coverage, the more difficult it is to avoid the running of ink in the high-coverage print areas (smudging). The thinner and finer the fabric, the lower the ink deposit, therefore, these fabrics are more suitabel for fine half-tone ruling.
Polyester Filter Mesh
Specification: DPP7-DPP165 (18-420 mesh)
Basic Information
Materials:
Polyester is also called polyester (PET) material
Colour:
white, yellow, black, or customized
Weave Type:
Plain weave, Twill weave, Dutch weave
Roll Length:
30-100m/Roll, Fixed Length, or customized
Polyester Filter Mesh Advantages:
Good acid resistance,
Temperature resistance,
Wear resistance,
High tensile strength, Low-elongation
Easy cleaning, good air permeability
Monofilament mesh is woven from yarn that is extruded from heated polyester into a single strand conventional monofilament. Polyester screen fabric will elongate under tension: the higher the tension level, the more the thread can stretch. At excessive tension levels, the thread reaches its “plastic deformation” point, and the screen will no longer hold tension
Polyester Filter Mesh
Specification: DPP7-DPP165 (18-420 mesh)
Basic Information
Materials:
Polyester is also called polyester (PET) material
Colour:
white, yellow, black, or customized
Weave Type:
Plain weave, Twill weave, Dutch weave
Roll Length:
30-100m/Roll, Fixed Length, or customized